The Enemy Attack Drone Costs $2,000. We Help Take Cost Out of the Hardware Built to Stop It.
Fathom Builds the Mechanical Hardware Behind Every Layer of the Kill Chain
Counter-drone programs are moving from qualification lots to rate production faster than almost any category in defense. Interceptors are bought by the thousand while turrets, radars and lasers ramp at the same time, and every new threat sends another revision back through the shop.
What slows integration is rarely the seeker or the software. More often it is a launcher detail, a cold plate or a sensor mount that could not keep up with the rate or the revision.
Fathom makes that hardware. We don’t make energetics, seekers or electronics, and we don’t take over your final integration. We make the machined, formed, molded, etched and printed parts that hold it all together, plus the fixtures your line needs to build it at rate.
That covers launcher and interceptor hardware, turret cradles and mounts, radar backplates and gimbal housings, laser beam director structures and cold plates, RF enclosures and EMI shields, rugged compute chassis, vehicle sleds and integration kits.
-
Rugged hardware. Parts built to survive the shock, vibration, EMI and weather your system is qualified against. Dimensional inspection and lot traceability come with every order.
-
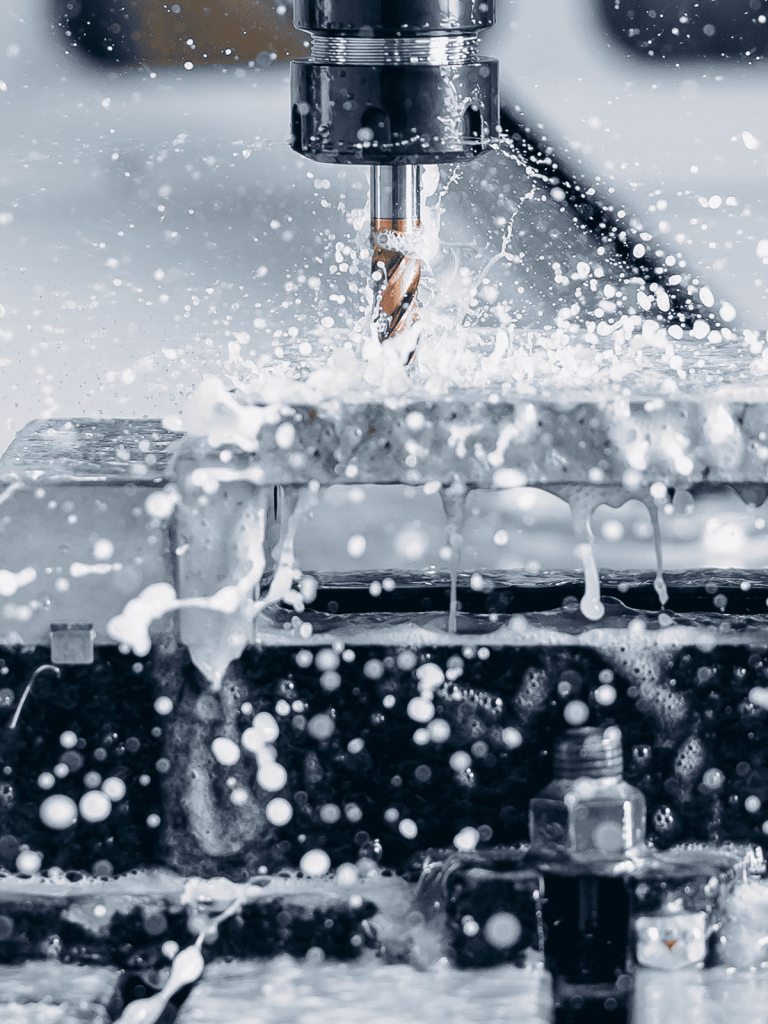
Fast revisions. Quick-turn additive and CNC parts with first article documentation, so a threat-driven ECO doesn’t stall your next test event.
-
Prototype to rate under one roof. Additive and urethane parts for early lots, then molded, machined and formed parts at volume. Your hardware scales without a supplier change.
-
Domestic and documented. Seven U.S. facilities with AS9100D, ISO 9001:2015 and ITAR registration (certifications vary by location). CMMC Level 2 is in process.
Defense-Grade Credentials With Startup Agility

6300+
30+

AS9100D

ITAR
Defense-Grade Quality at the Speed Counter-Drone Programs Move
Most contract manufacturers pitch a counter-drone OEM on building the effector, the sensor or the whole system. Those are the things you will never hand over.
Fathom is the mechanical layer around them. Four things set us apart from other contract manufacturers:

Domestic, ITAR-Registered Manufacturing Across Seven U.S. Facilities
Prototype and Rate Processes Under One Roof
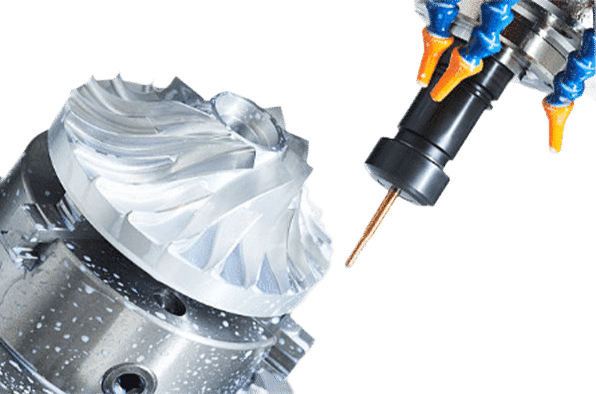
With 30+ manufacturing technologies, we can move a part from additive or urethane to molded, machined or formed production. Your hardware scales without changing suppliers.
Engineer-Reviewed DFM on Every Quote
Our engineers flag cost, tolerance and process issues before the quote goes out, including design-to-cost moves like castings to machined-from-plate. You find the savings at print review, not at first article.

A Single Point of Contact Across Every Site
Our Program Management Office coordinates machining, sheet metal, additive, molding, finishing, assembly and kitting across sites. That means fewer POs, audits and handoffs across a multi-effector system.
Defense-Grade Quality at the Speed Counter-Drone Programs Move
Most contract manufacturers pitch a counter-drone OEM on building the effector, the sensor or the whole system. Those are the things you will never hand over.
Fathom is the mechanical layer around them. Four things set us apart from other contract manufacturers:
-
Domestic, ITAR-Registered Manufacturing Across Seven U.S. Facilities
Mechanical content around your seekers, sensors and effectors stays in the U.S., with material traceability to support DFARS requirements. Offshore sourcing is reserved for non-sensitive parts where program rules allow.
-
Prototype & Rate Processes Under One Roof
With 30+ manufacturing technologies, we can move a part from additive or urethane to molded, machined or formed production. Your hardware scales without changing suppliers.
-
Engineer-Reviewed DFM on Every Quote
Our engineers flag cost, tolerance and process issues before the quote goes out, including design-to-cost moves like castings to machined-from-plate. You find the savings at print review, not at first article.
-
A Single Point of Contact Across Every Site
Our Program Management Office coordinates machining, sheet metal, additive, molding, finishing, assembly and kitting across sites. That means fewer POs, audits and handoffs across a multi-effector system.
Your Expert Aerospace & Defense Team
Andrew Sonier
Adam Villarreal
Sebastian
Wasikowski
Mark Huffman
Ryan Uecker
Trey Harper
Interceptor Output That Scales Without Adding Suppliers
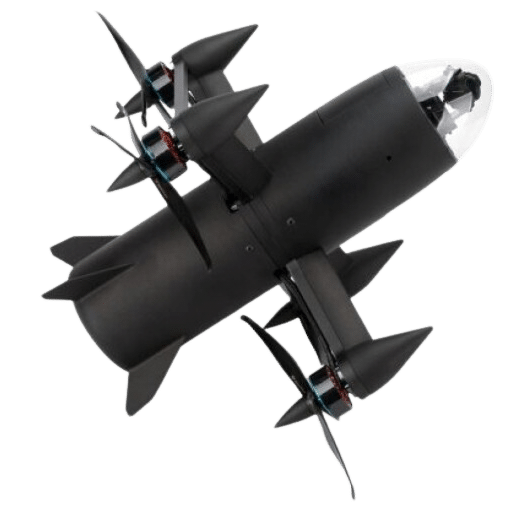
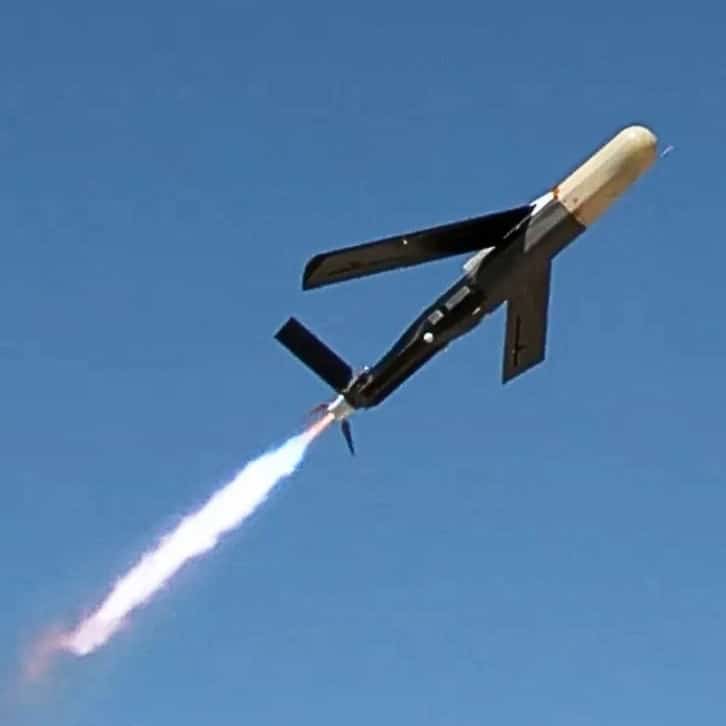
Interceptors are the highest-volume hardware in the kill chain. Output once measured in dozens is now measured in hundreds a month, and cost-per-kill targets push every round toward machined aluminum, sheet metal, molded and additive parts.
Fathom builds the non-energetic content: fuselage sections, fins and control-surface details, bulkheads, seeker and electronics housings, nose cones, launch tubes, canisters, launcher racks and the fixtures that assemble them.
-
Airframe and structure: Fuselage sections, bulkheads, hardbacks and fin details from high-volume CNC in Minneapolis, MN and Hartland, WI.
-
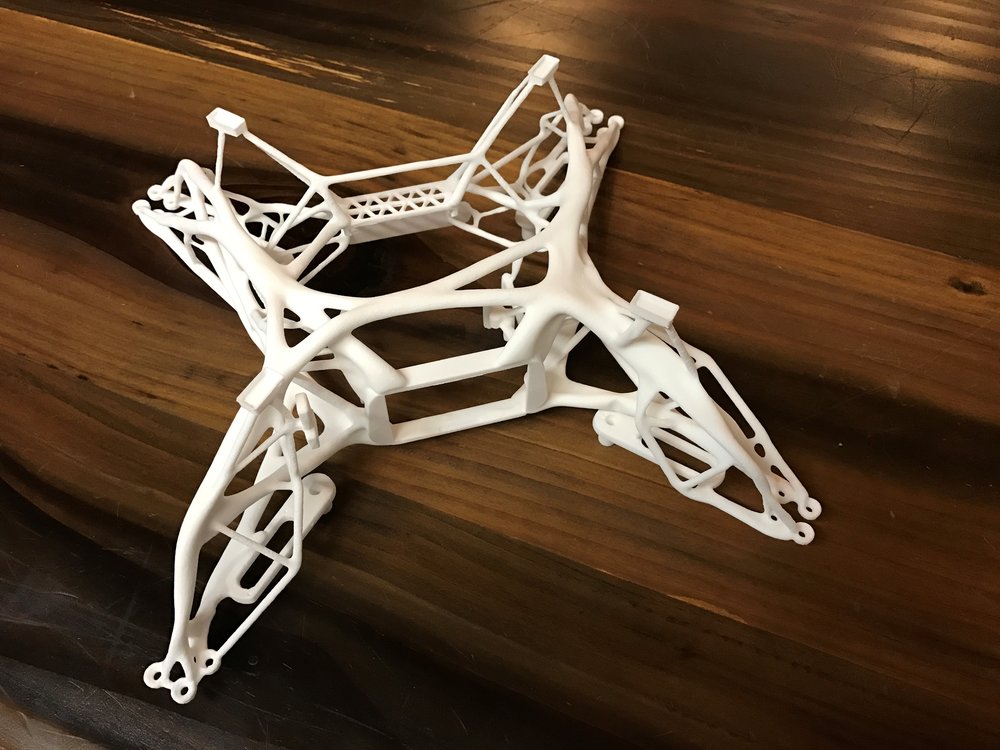
Attritable and early-lot parts: SLS and MJF airframe parts and brackets plus urethane bridge tooling from Hartland, WI, with a planned move to injection molding at rate.
-
Launch hardware: Launch tubes, canisters, launcher racks and multi-round pods from sheet metal and fabrication in Denver, CO and Ithaca, NY.
-
Documented at volume: AS9102 first article, weight and balance control and lot traceability, with assembly fixtures kitted by build station.
Turret Production That Ramps Without Waiting on Forgings
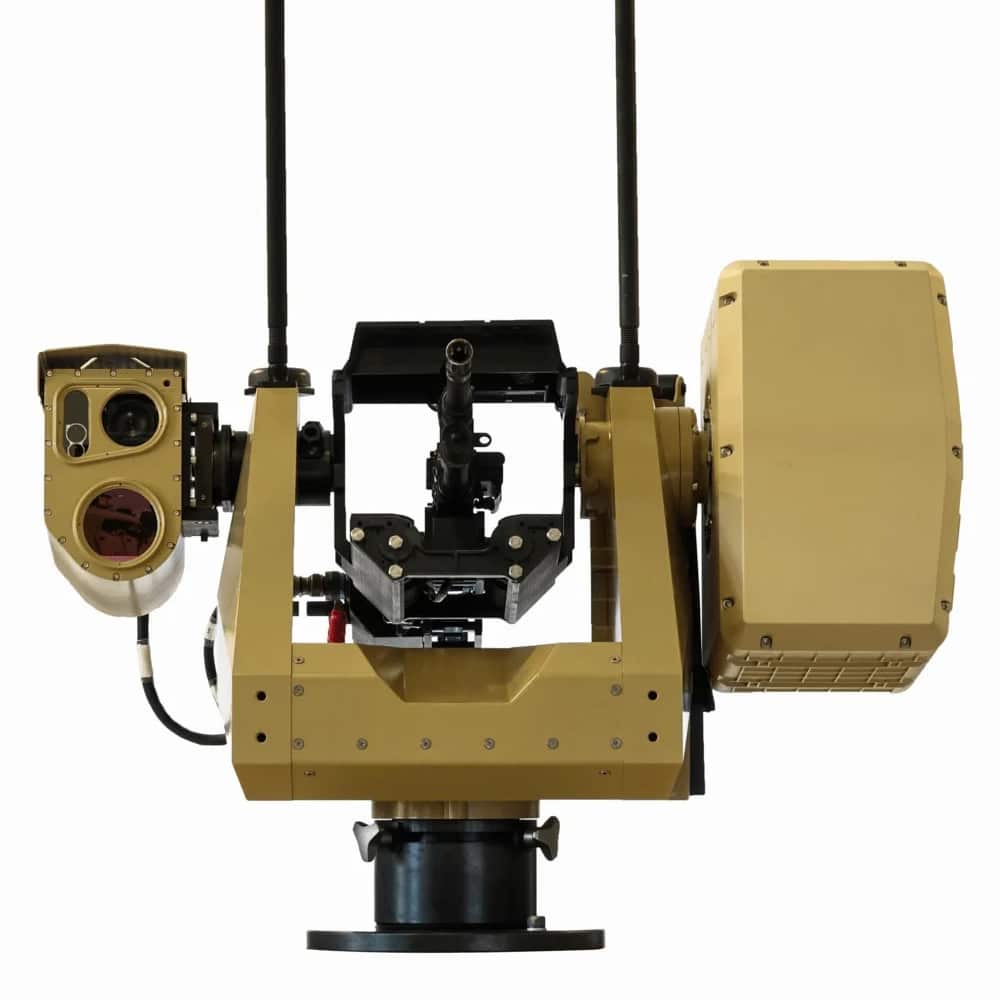
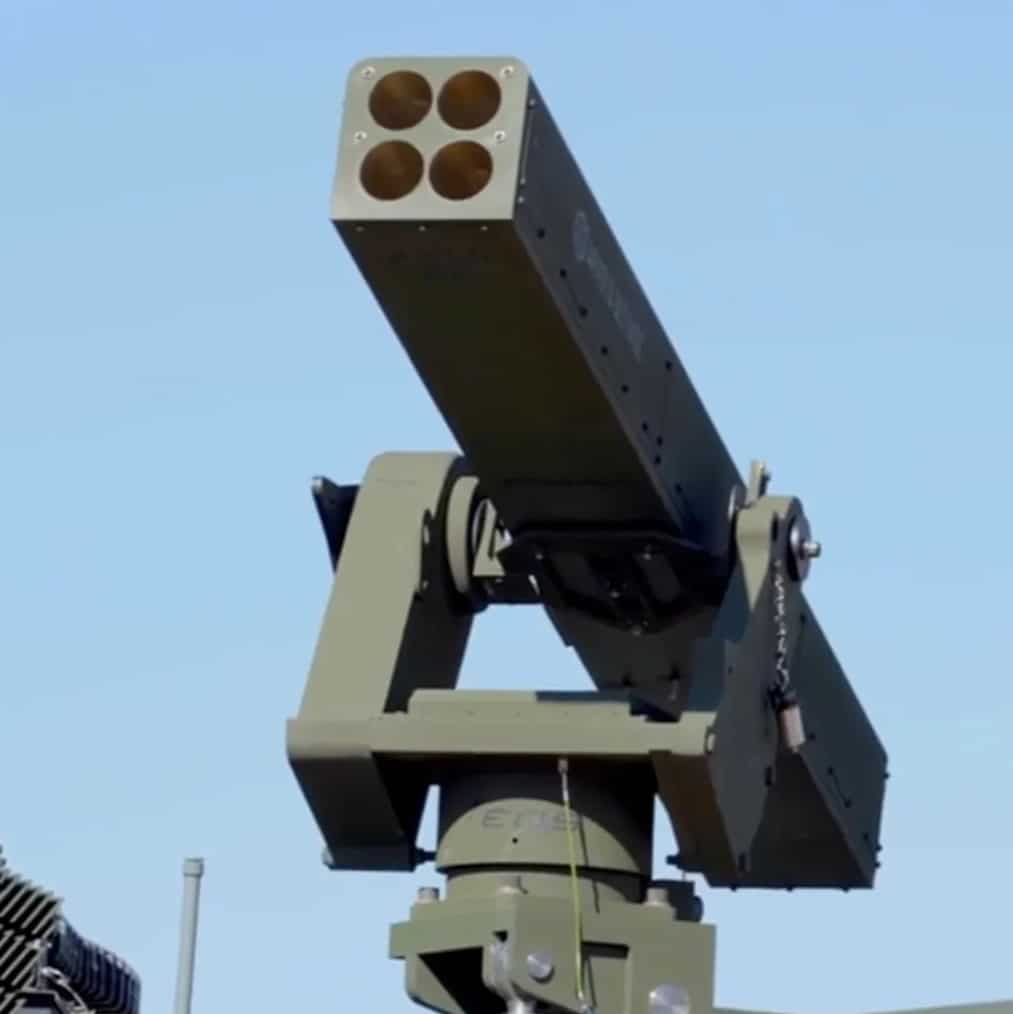
Gun-based defeat is in production and ramping, from 30mm proximity-round systems to autonomous turrets and remote weapon stations. Each system carries heavy machined and fabricated content, and casting and forging capacity is tight enough to pace an entire program.
Fathom builds turret ring and slew-bearing housings, elevation cradles, gun mounts and adapters, ammunition cans, feed chutes, sensor and sight housings, drive housings, shields and covers, with machined-from-plate alternatives when forgings won’t arrive in time.
-
Large machined structures: Turret ring housings, elevation cradles, gun mounts and adapters from large-envelope 5-axis and horizontal CNC in Minneapolis, MN.
-
Fabricated content: Ammunition cans, feed chutes, shields and covers from welding and sheet metal in Denver, CO.
-
Sensor and drive details: Sight and sensor housings, drive housings and turned details, finished in hard anodize, phosphate or CARC.
-
Serialized and compliant: DFARS specialty metals traceability and serialized inspection across hundreds of systems and their spares.
Sensor Production That Keeps Pace With Every Site, Vehicle & Handheld
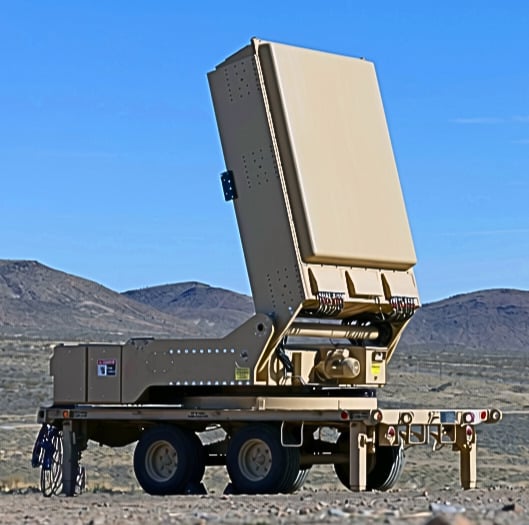
Detection is the most mature and most repeated layer. Every fixed site, vehicle and handheld system needs radar, RF or EO/IR hardware, and sensor makers are building factories sized for thousands of units a year. Homeland and critical infrastructure buyers add volume on top of military demand.
Fathom builds radar array backplates, cold plates, radome and housing details, pan-tilt heads, masts, mounting brackets, EO/IR gimbal housings and window mounts.
-
Precision array hardware: Radar backplates held to tight flatness, plus gimbal ball housings, from 5-axis CNC in Minneapolis, MN and Hartland, WI.
-
Thermal parts: Cold plates and heat exchangers, including DMLS conformal cooling designs from Hartland, WI.
-
Shields and flats: Photochemically machined EMI shields, gaskets and thermal spreaders from Newark, NY.
-
Masts, mounts and enclosures: Sealed enclosures, masts and pan-tilt brackets from Denver, CO, with non-ITAR commercial variants from Austin, TX.
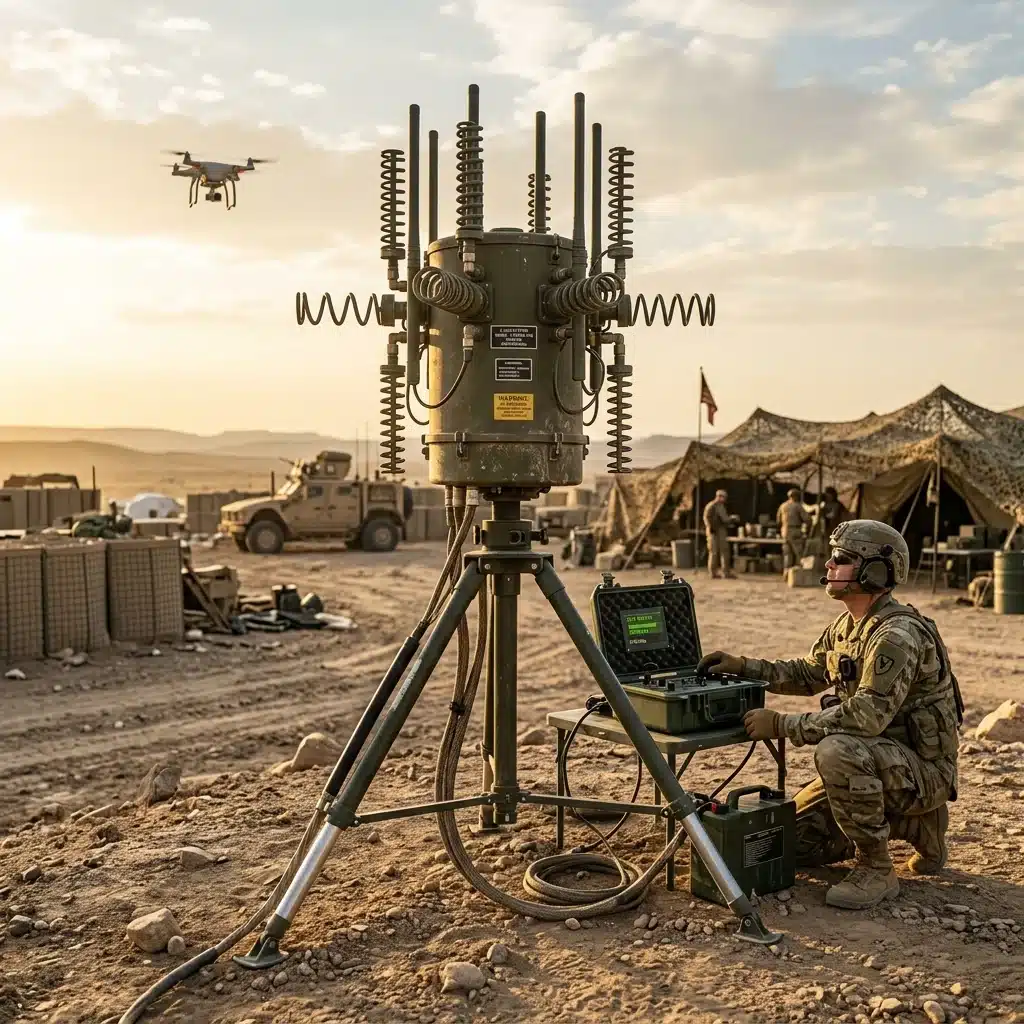
RF Defeat Hardware at Handheld Volume, HPM Hardware at First Production
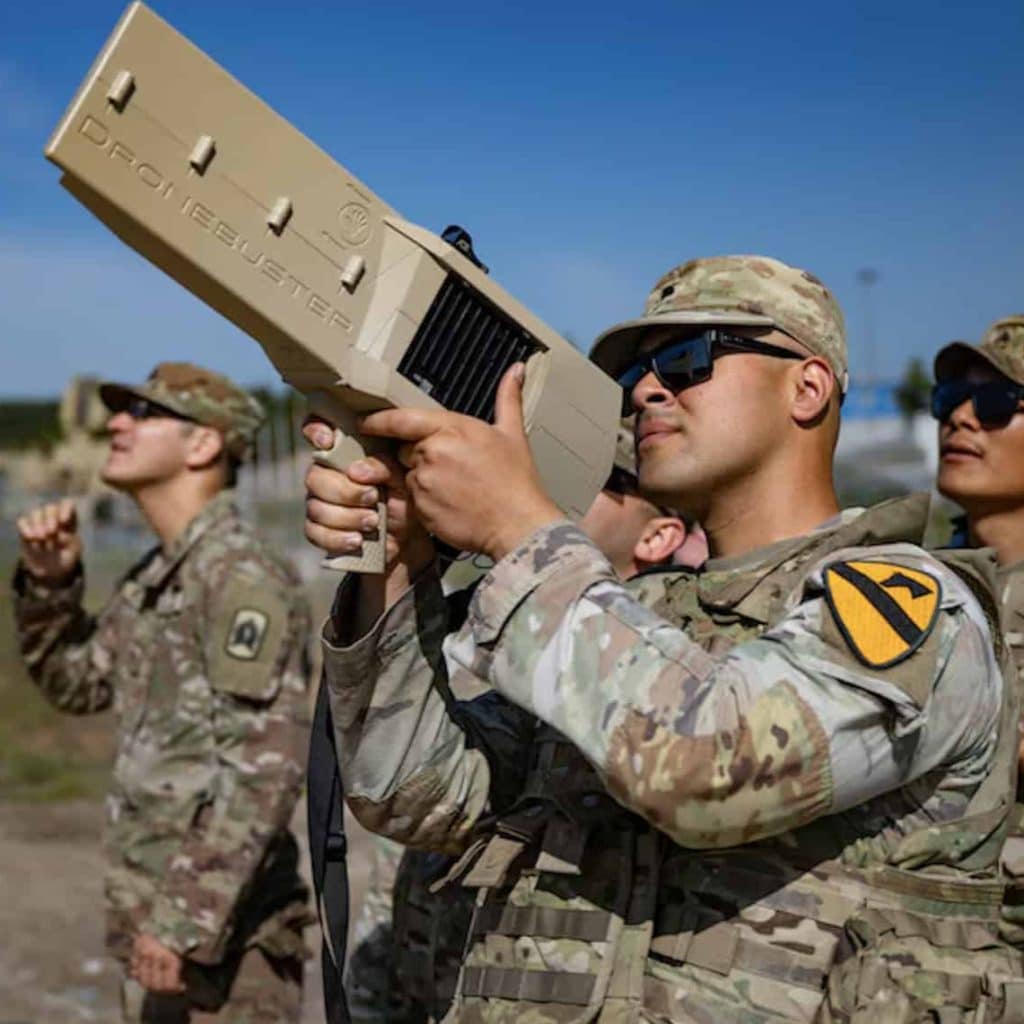
RF jamming is the most widely fielded layer, and high-power microwave is moving from prototypes to production-representative systems. Both need shielded enclosures, antenna hardware and thermal parts, and handheld systems bring unit volumes in the thousands.
Fathom builds handheld jammer housings and grips, antenna shrouds, battery pack housings, sealed RF enclosures, EMI shields and gaskets, masts, finned heat sinks, HPM amplifier module housings, cold plates and trailer integration hardware.
-
Handheld housings: MJF and urethane-cast housings for early lots, then injection molding at volume from Hartland, WI.
-
RF enclosures: Sealed sheet metal and machined aluminum chassis with conductive finishes from Denver, CO and Ithaca, NY.
-
EMI and thermal details: Photochemically machined shields, gaskets and shims from Newark, NY, plus finned heat sinks and cold plates.
-
HPM integration: Repeat-build amplifier module housings and cold plates for systems that carry well over a hundred modules each, plus trailer integration hardware.
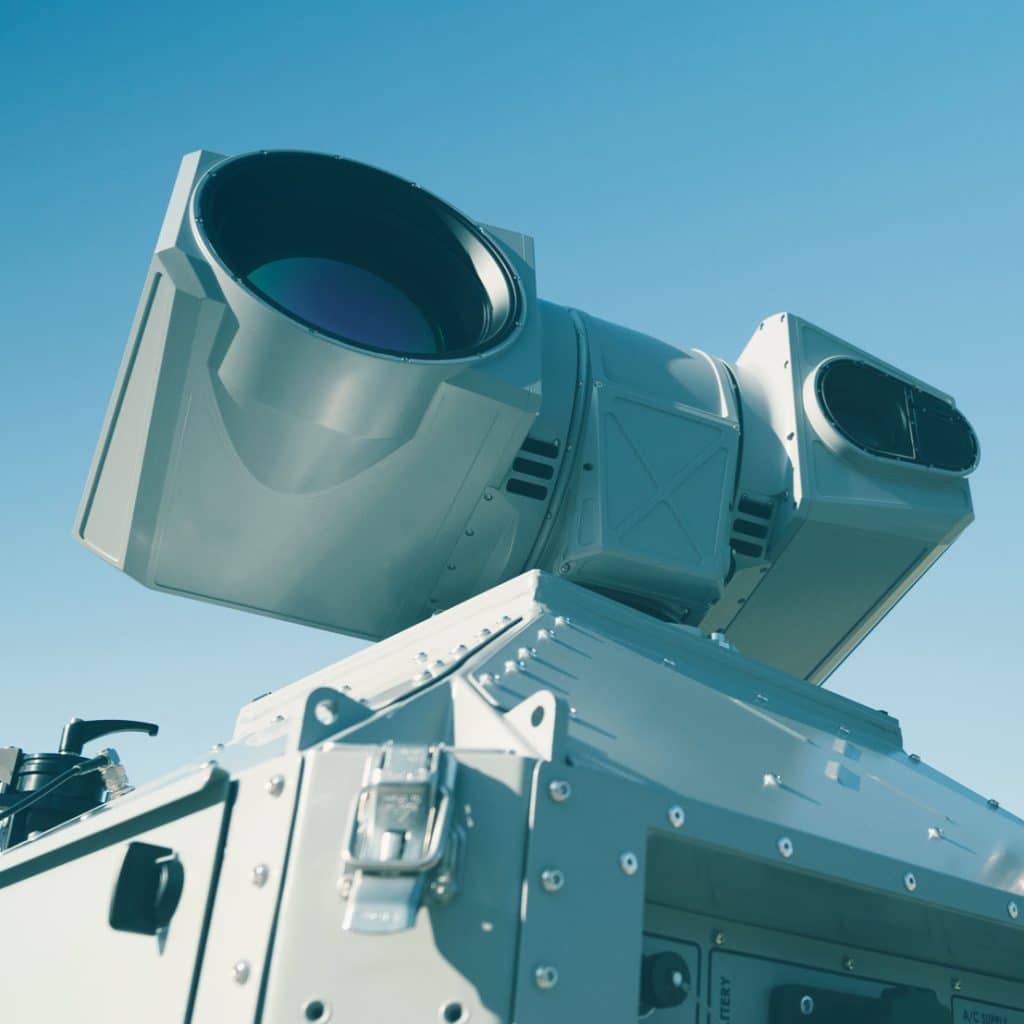
Laser Programs That Move From Demonstrator to Production on Schedule
Tactical lasers are entering first production. Most of their mechanical content sits in the beam director, thermal system and vehicle integration rather than the laser source, and beam control, thermal management and SWaP are the risks programs flag first.
Fathom builds beam director housings, azimuth and elevation gimbal yokes, optical bench and mirror-mount details, cold plates, coolant manifolds, heat exchangers, power enclosures, pallet frames and vehicle mounting kits.
-
Precision optical structures: Beam director housings, gimbal yokes and optical bench details from stress-relieved 5-axis CNC and wire EDM in Hartland, WI and Minneapolis, MN.
-
Thermal management: DMLS conformal cold plates, coolant manifolds and heat exchangers from Hartland, WI.
-
Low-CTE details: Mirror mounts and precision details in Invar and titanium with material certs and flatness and bore verification.
-
Power and integration: Battery and power enclosures, pallet frames and vehicle mounting kits from fabrication and assembly in Denver, CO.
Vehicle-Integrated Kill Chains Without Supplier Sprawl
Command and control is now bought as its own layer, and it ships on rugged hardware that scales with every fielded system. On a vehicle, that hardware shares a sled or pallet with radar, EW, guns and interceptors, and each layer brings its own shops, POs and audits.
Fathom builds rugged compute chassis and ATR boxes, 19-inch rack enclosures, operator console panels, display and tablet mounts, cable brackets, transit case inserts, shelter kits, sleds, pallets and adapter kits.
-
Rugged compute: Sheet metal and machined heat-sink chassis, ATR boxes and rack enclosures from Denver, CO and Ithaca, NY.
-
Operator hardware: Console panels, molded bezels, display and tablet mounts, cable brackets and transit case inserts.
-
Vehicle integration: Sleds, pallets, adapter kits and mounts for multi-vehicle fits, with powder coat or CARC, hardware insertion and electromechanical assembly in Denver, CO.
-
One point of contact: Our Program Management Office coordinates every site, so a multi-effector system arrives kitted and documented.
Same-Day Answers From an Engineer Who Signed Off on the Print
Fathom isn’t a transactional machine shop. We’re not a broker sending automated quotes and generic DFM feedback, either. On hardware that has to survive shock, vibration, EMI and weather in the field while the threat keeps changing, our human-first approach is what makes the difference.
Our engineers review your prints for tolerance stack-up, flatness on array and optical mounts, thermal paths, EMI sealing, coating stack-up, weight and design-to-cost opportunities. Problems surface at print review instead of at first article or a failed test event.
You get a named program contact instead of a ticketing queue, and an engineer on the phone the same day instead of three quote cycles later. Revision control, first article documentation and inspection packages are built into the flow rather than bolted on at the end.
So when a new threat forces a revision or a delivery order doubles, the mechanical layer absorbs it instead of resetting your schedule. That’s white-glove service applied to defense-grade manufacturing, and it’s why fast-moving defense programs keep coming back to Fathom.